






What causes gold loss in a gold mining dredge recovery circuit
Gold loss in a recovery circuit is rarely caused by one dramatic failure. In a gold mining dredge, losses usually begin when the circuit is asked to treat material that it has not properly liberated, classified, or presented to the recovery equipment. Fine gold can leave with tailings, coarse gold can bypass a screen or sluice, and gold locked in clay can travel through the plant as waste even when the dredge appears to be operating at full capacity.
The first task is to identify where the loss occurs. Sampling only the final concentrate can confirm that gold is being recovered, but it cannot show whether the recovery circuit is losing value in oversize discharge, trommel undersize, sluice tailings, or a bypass line. A short, controlled sampling program at each transfer point is often more useful than making broad changes to water flow or feed rate.
Clay and poor liberation send gold through the plant
Sticky clay is one of the most common reasons for poor recovery in dredged placer material. Gold trapped inside clay balls may never reach the sluice or other gravity concentrator as free particles. Instead, it can be carried out with oversize reject or discharged with muddy tailings. This problem becomes more severe when the feed contains roots, organic material, compacted riverbed layers, or weathered cemented gravel.
More water alone does not always solve it. Excessive flow may wash material through the circuit before scrubbing is complete, while insufficient water leaves clay intact and causes screen blinding. Operators should watch the discharge from the trommel or scrubber: visible clay balls, coated pebbles, and uneven slurry generally indicate that the material is not being properly broken down before recovery.
A circuit needs enough residence time and agitation to liberate gold without turning the feed into an uncontrolled high-volume slurry. Where material changes across the mining face, settings that worked on loose sand may fail quickly in clay-bearing zones. Feed rate, wash-water pressure, drum speed, and screen condition should be adjusted together rather than one at a time.
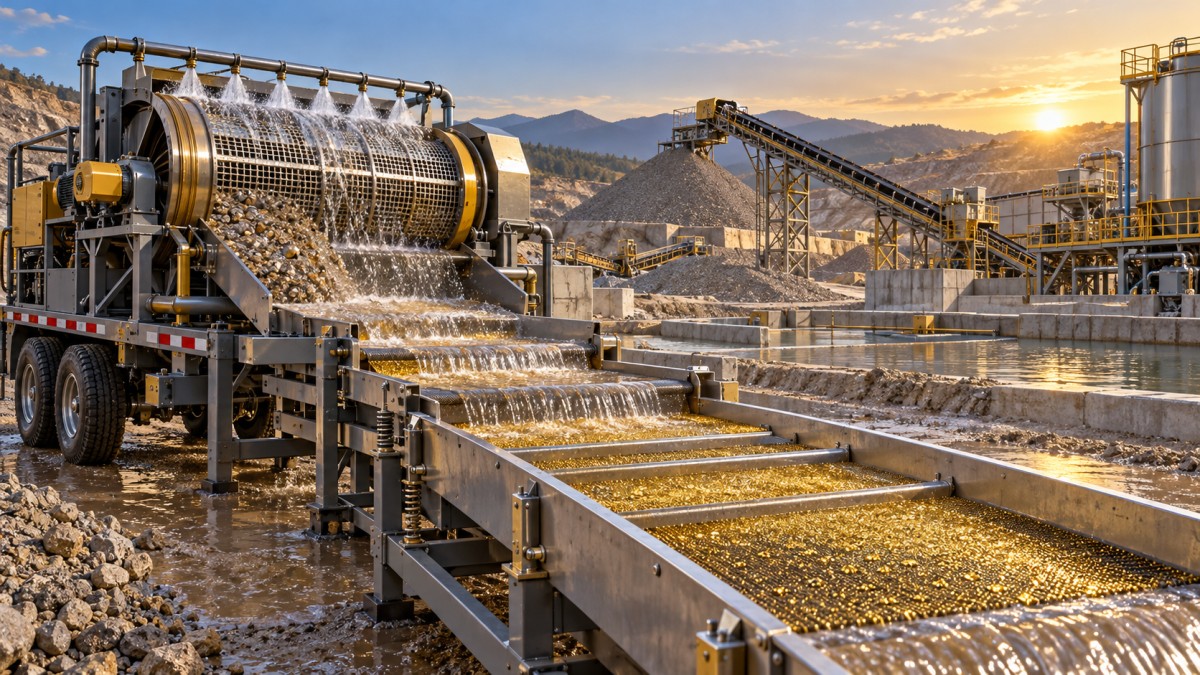
For small, moving operations, a Movable Gold Trommel Washing Plant can be relevant where the feed requires both scrubbing and screening before gravity recovery. Its practical value depends less on mobility itself than on whether the hopper washing, drum scrubbing, screen apertures, and recovery section are matched to the actual material being excavated.
Incorrect classification overloads the recovery section
Gravity recovery equipment works best when particle size and slurry conditions are reasonably controlled. If oversize rocks, wood, compacted clay, and too much fine slurry all arrive together, the recovery section must process a wide and unstable feed. This can disturb the bed in a sluice, cover gold-trapping carpet with coarse material, or create fast channels that carry fine gold directly into tailings.
Screen selection is therefore a recovery decision, not simply a throughput decision. An aperture that is too large can send excessive coarse material downstream and make the sluice difficult to control. An aperture that is too small may reject gravel containing coarse gold or become blinded by clay, forcing water and slurry to bypass the intended route.
Before changing screen size, operators should establish the size range of the gold they are trying to recover. A circuit designed around visible coarse flakes may lose a large amount of fine or flat gold even though its concentrate looks satisfactory. Conversely, a fine-gold-focused setup can become unstable when oversized gravel repeatedly enters the recovery zone.
- Inspect trommel panels for worn openings, broken sections, and local blinding.
- Check that oversize discharge is not carrying unwashed clay, gravel, or recoverable coarse gold.
- Confirm that all undersize slurry reaches the recovery equipment rather than escaping through leaks or emergency bypasses.
- Review feed consistency when the dredge moves from loose sediment into compacted or mixed ground.
Water velocity can either expose gold or wash it away
Sluice losses are often blamed on the carpet or riffles, but unstable water and slurry conditions are frequently the underlying cause. If velocity is too high, fine gold and thin flakes may remain suspended and leave with tailings. If velocity is too low, heavy black sand and coarse waste can pack the recovery surface, preventing gold from settling into the trapping media.
Water distribution matters as much as total water volume. A partially blocked spray bar, an uneven manifold, or a misaligned feed box can create one high-energy channel and several low-energy zones. Material then crosses the sluice unevenly: one section scours clean while another fills with sand. Looking at the surface during operation often reveals this problem faster than checking pump pressure alone.
Operators should also avoid treating a clean-looking sluice as proof of good recovery. A surface that is being aggressively washed may look efficient while fine gold is being carried off. Tailings checks made after a change in pump speed, dredge production rate, or water source condition are necessary to judge whether the adjustment improved recovery or simply increased throughput.
Feed surges and bypasses create losses that are easy to miss
A gold mining dredge does not always deliver uniform feed. Sudden excavation of a gravel pocket, a collapse of bank material, or an operator increasing suction to clear a blockage can send a large surge through the circuit. The screen and recovery unit may then receive more solids than they can process, causing material to overflow, short-circuit, or pass over the recovery surface too quickly.
These events are especially damaging because they may be intermittent. Daily production can look normal while a few short overloads account for a meaningful share of lost gold. Monitor hopper level, slurry density, screen discharge, and recovery-box behavior during the most variable periods of the shift, not only during stable running.
Unplanned bypasses deserve the same attention. Leaking chutes, worn seals, split hoses, blocked screens, and overflow routes can all create a path around the gold-saving equipment. Any material path that is difficult to sample is a potential blind spot. When a recovery problem appears suddenly after maintenance or relocation, inspect these physical routes before making major process changes.
Fine gold requires a separate recovery mindset
Coarse gold settles quickly and is relatively forgiving. Fine, flat, or flour gold is less forgiving because it responds strongly to water velocity, slurry density, surface condition, and turbulence. A circuit can recover coarse visible gold well while losing a substantial fine fraction. This is why visual inspection of concentrate alone is not enough to assess performance.
Where tailings contain fine gold, reducing feed rate and stabilizing water distribution is often a better first response than adding more aggressive wash water. The recovery surface should be inspected for loading, flattening, damage, or poor contact between the slurry and trapping material. Fine-gold recovery also depends on keeping the recovery unit clean enough to retain gold while avoiding overly frequent cleanups that interrupt stable operation.
A disciplined test should change one operating variable at a time, then compare samples from the same material zone. Altering drum speed, water flow, feed rate, and recovery media together may produce a better or worse result, but it will not show which change caused it.
Start with material balance, then adjust the dredge
When gold loss is suspected, begin with representative samples from feed, oversize, recovery tailings, and final concentrate. The purpose is not to chase a perfect laboratory-grade balance on the first day. It is to locate the largest escape route: unwashed oversize, poor liberation, unstable sluice conditions, or a physical bypass.
Once that route is identified, the next adjustment becomes clearer. Clay-related loss calls for better washing and scrubbing. Oversize loss calls for checking screen performance and reject handling. Fine gold in tailings calls for reviewing water distribution, feed loading, and recovery-surface condition. Treating all losses as a sluice problem can waste operating time while the real issue remains upstream.
Recovery performance should be checked again whenever the dredge moves into a different sediment layer, changes excavation method, receives new screen media, or undergoes a significant pump or piping repair. In placer work, the material controls the circuit as much as the machine does; the most reliable operators keep the circuit aligned with changing ground conditions.